Capabilities
Urethane Mold Design, Formulation, Molding and Machining
The team at Urethane Specialists handles every step of producing precision urethane parts in one Salinas plant. Urethane delivers superior engineering properties when the design, formulation, molding and machining are done right. Here is how we do it.
Mold Design
Steel and aluminum molds, cut on CNC mills and precision lathes from 3D drawings.
Formulation
Compounds matched to the application, 30A to 80D, with FDA compliant options.
Molding
Vacuum degassed, temperature controlled casting that produces void free parts.
Machining
Parts turned, deburred, balanced and polished to finished size, then inspected.
Step 1
Mold Design
Molds must reproduce challenging geometry and compound shapes, including cavities, sharp radii, fillets, ribs and recessed surfaces. That calls for careful prototyping and mold fabrication.
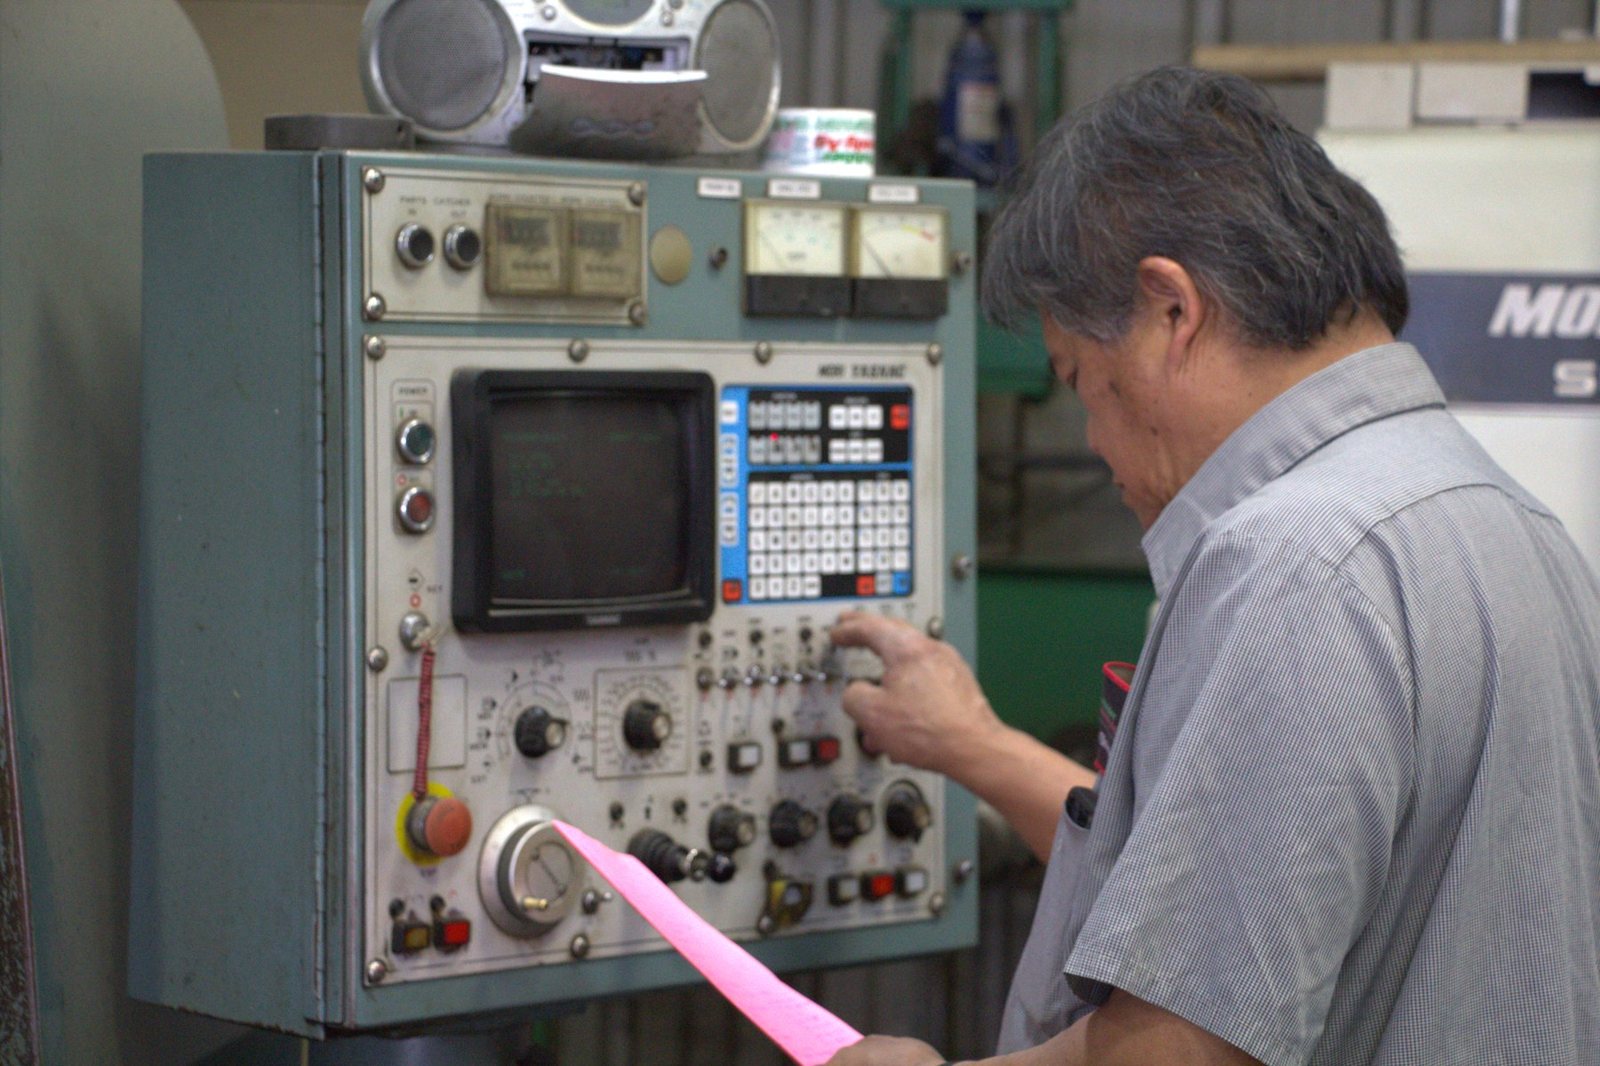
Complex mold shapes are milled out of steel or aluminum because of the heat and pressure involved in curing urethane, and because a mold has to withstand thousands of production cycles. Our mold work runs on 3D drafting, precision lathes and CNC mills to hold accuracy.
Molds are also designed so the part comes out cleanly once it has cured. Designers build in features such as draft angles, parting lines, side actions, bump offs and sliding shutoffs to handle undercuts, ridges and projections that would otherwise trap the part.
No mold for your part yet? We cut new molds in house. Once it exists, reorders run on the same tooling.
Step 2
Formulation
Polyurethane is versatile because of the almost unlimited number of formulations that can be tailored to a specific application. Additives let the formulator dial in the characteristics the part needs:
- Hardness, measured as durometer (see the scale)
- Resistance to abrasion, heat and chemicals
- Tensile strength
- Specific gravity and buoyancy
- UV light protection
- FDA compliant formulations for food contact
We formulate and blend our own compounds in Salinas, so the part is built for the environment it runs in: chlorinated washdown, acidic produce, water, heat, oils, or dirt and rock.
Step 3
Molding
The goal of the molding process is a casting that has the specified engineering properties and is free of voids, air pockets and other imperfections.
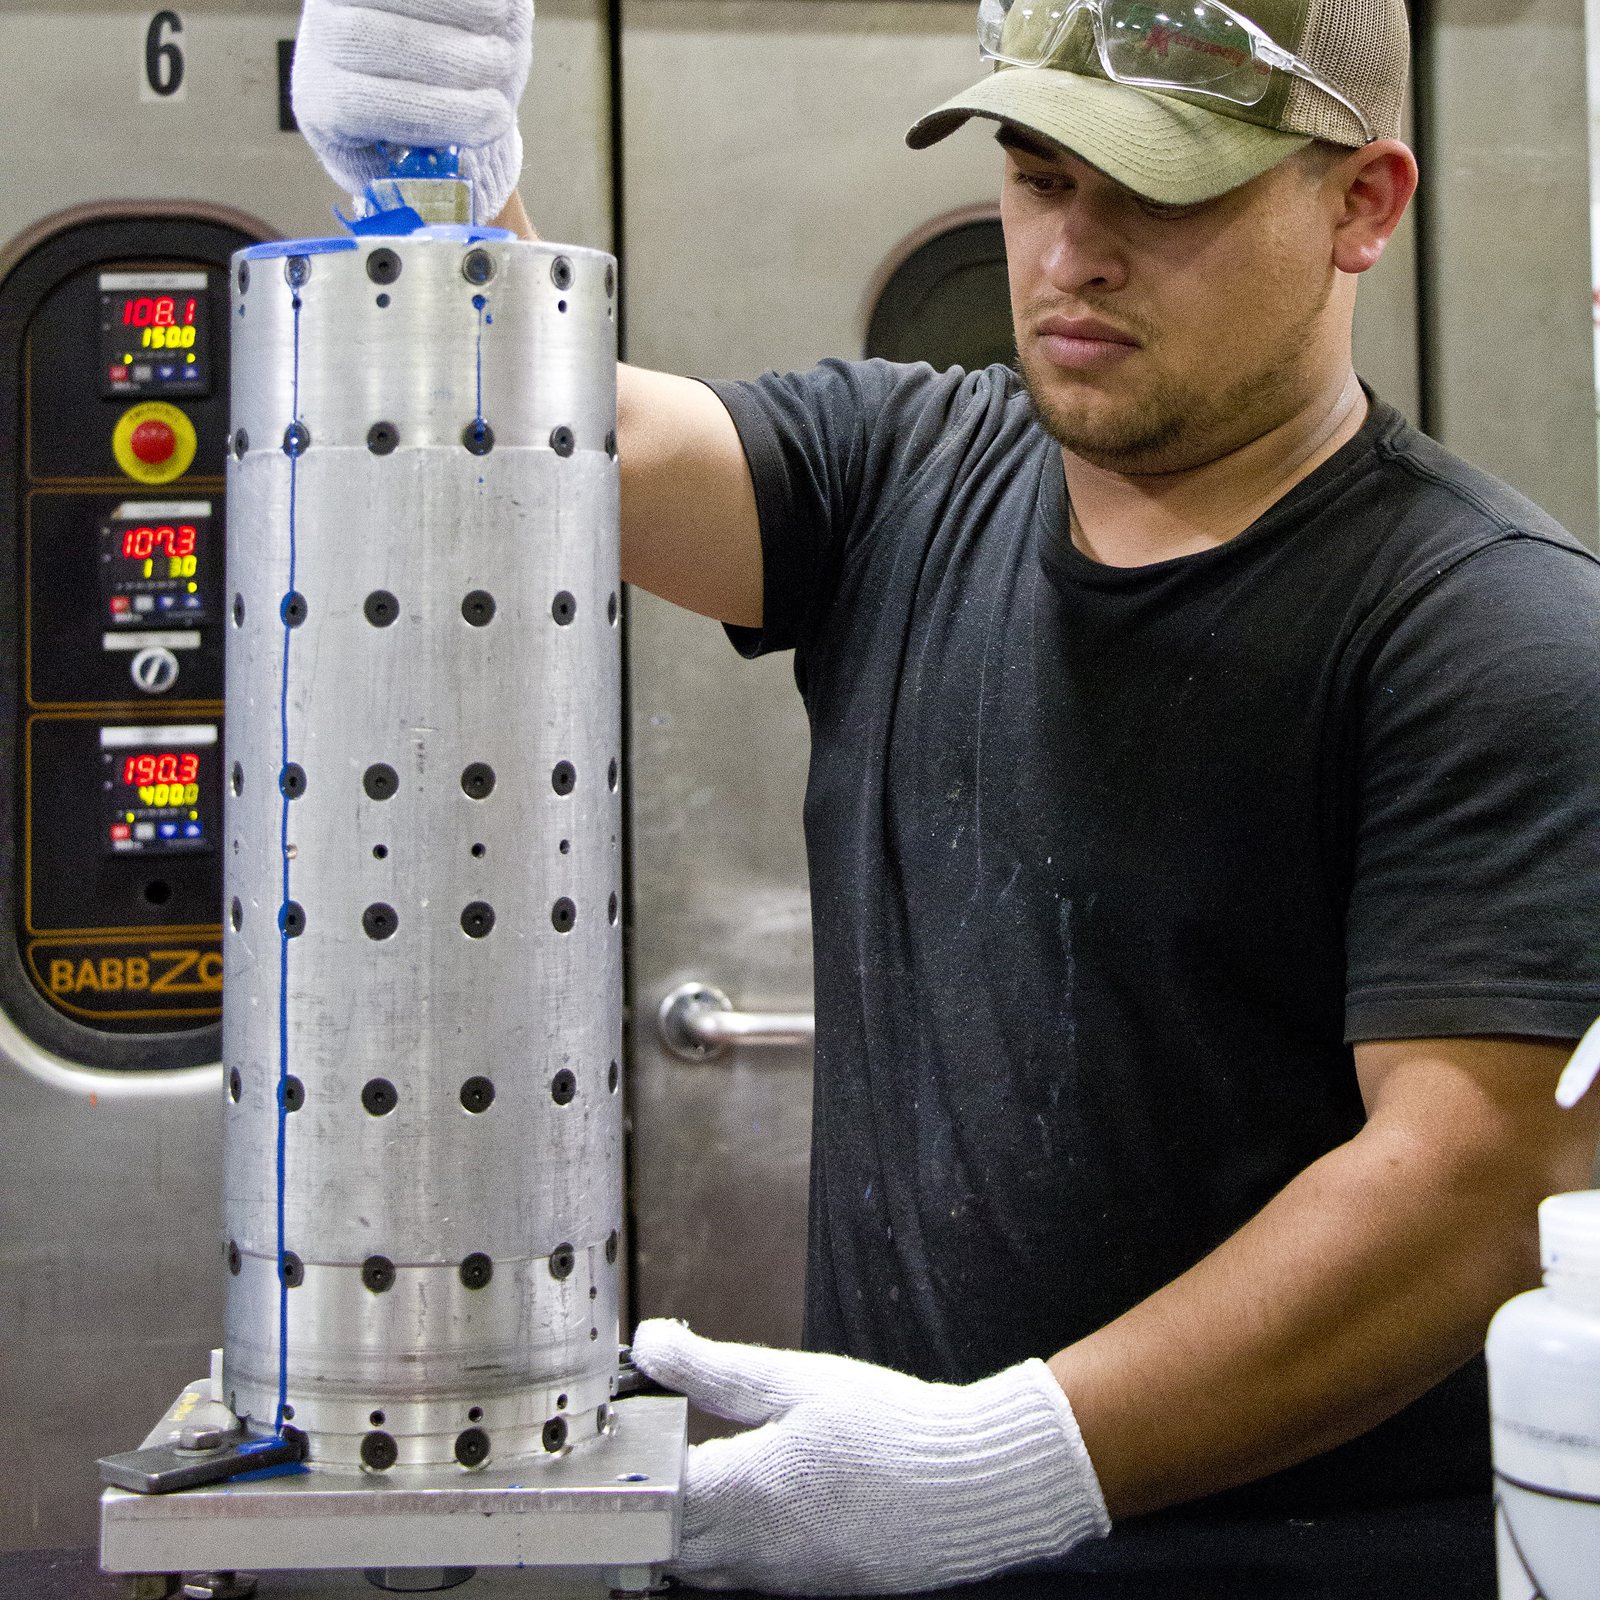
Metal molds are first brought to a precise temperature in industrial ovens. The liquid urethane is then mixed with the additives and curatives the formulation calls for. Because the curative starts the hardening reaction, the clock begins ticking the moment it goes in.
The mix goes into a vacuum chamber to pull out air introduced during mixing. Bubbles would leave voids that weaken or unbalance the finished part. Operators then transfer the urethane to the heated molds without introducing new air, and the cure is timed and monitored over hours or days to hit the right heating and cooling cycle.
Step 4
Machining
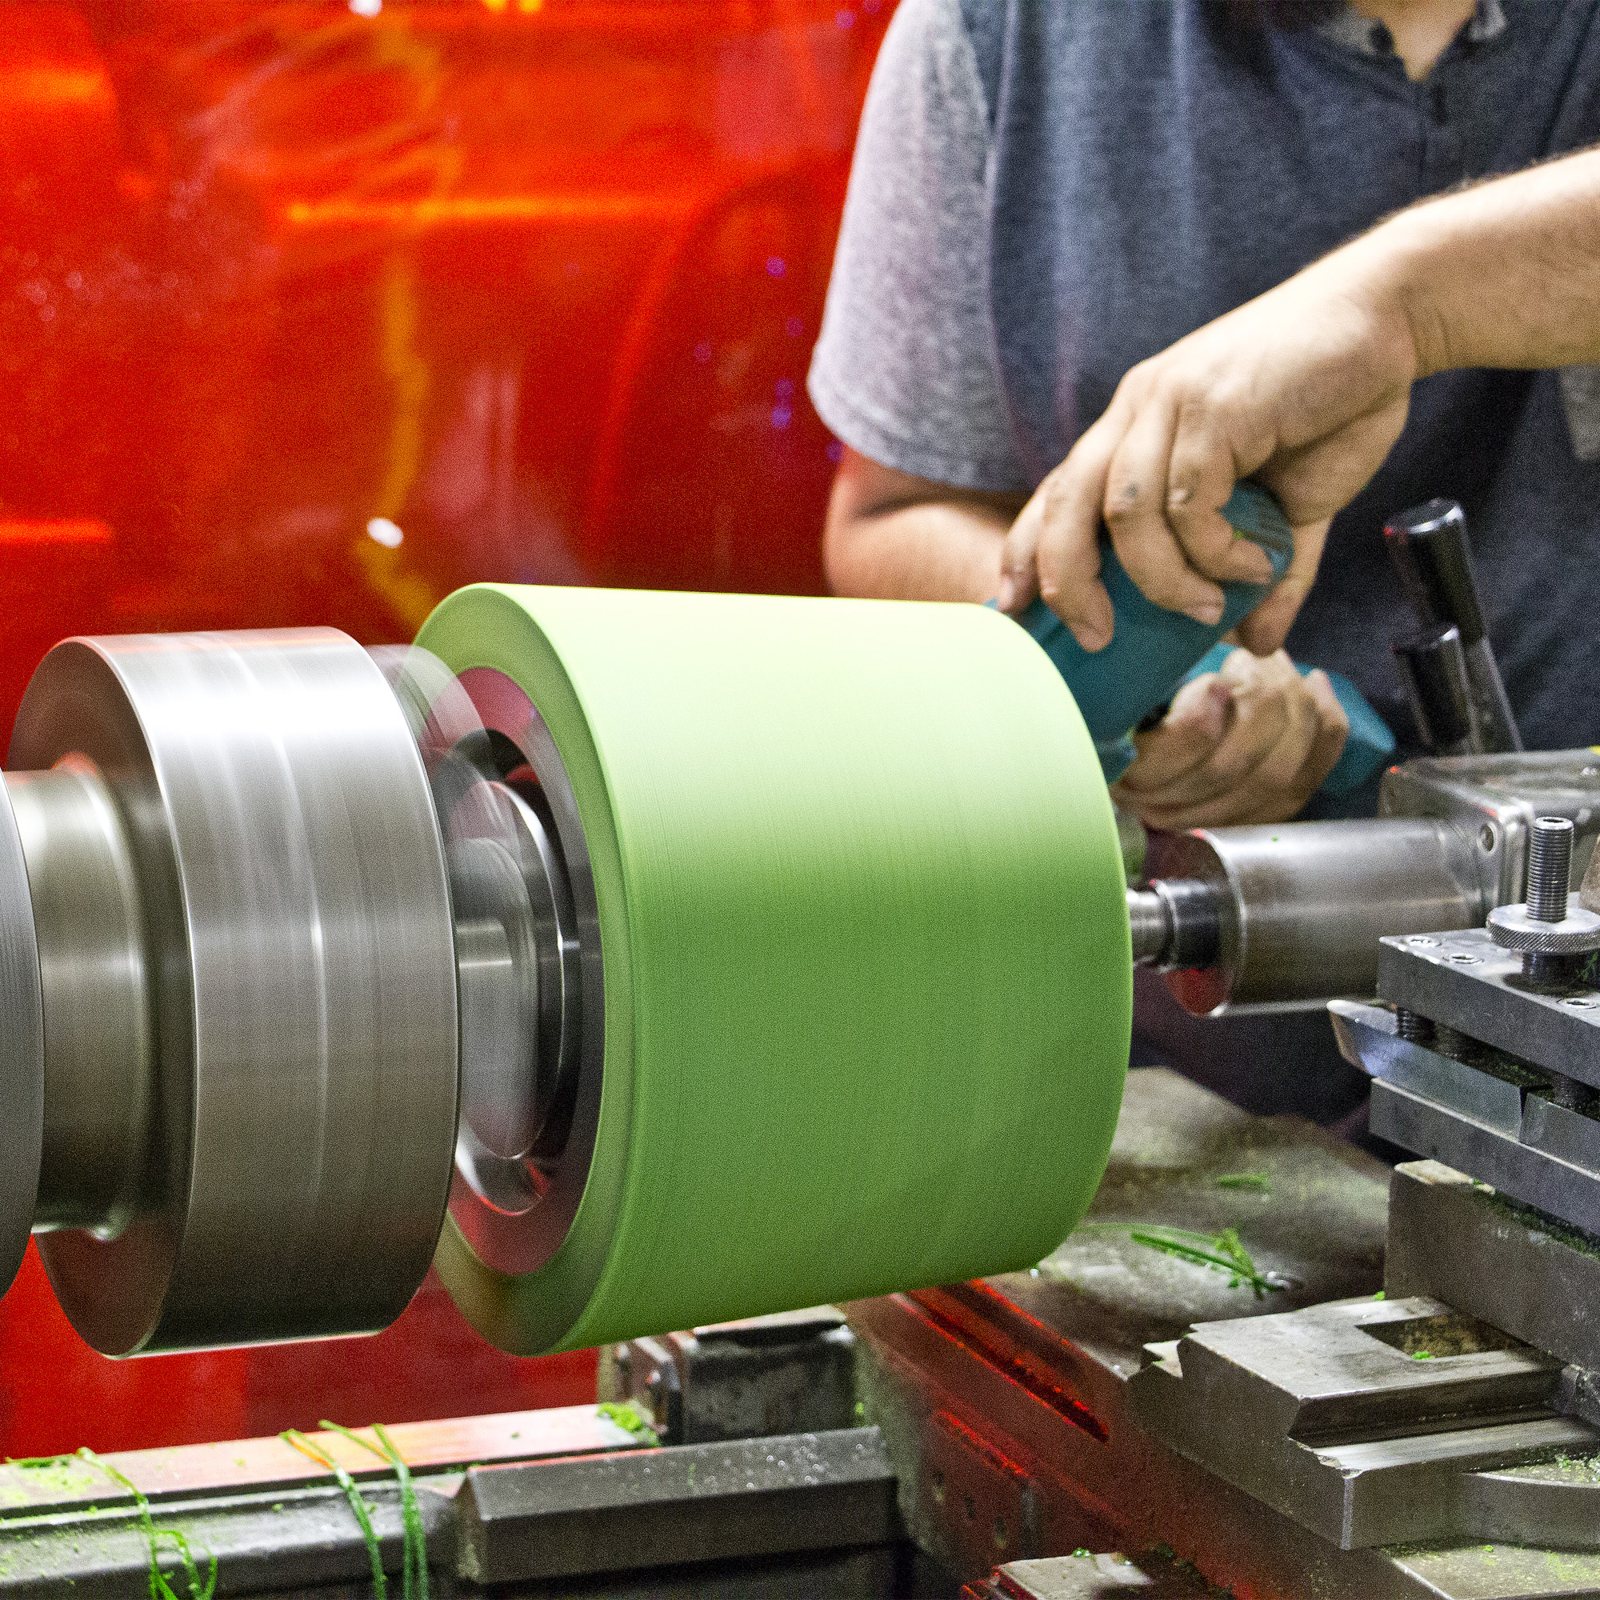
Parts come out of the mold once the urethane has cooled. They are then turned on a lathe to be deburred, balanced and polished to finished size. Where the mold cannot produce a feature, we add textures, grooves, ridges and other details on the machine.
We also make cores and shafts in house, press bearings, and strip and recast worn rollers and wheels on the customer’s own core. Every part goes through quality control inspection before it ships or is staged for pickup at a Green Rubber Kennedy Ag branch.
Choosing a hardness
What does durometer actually feel like?
Durometer is how hard a urethane is. Flexible parts are measured on the Shore A scale, rigid parts on Shore D. Here is the range we cast, next to things you already know.
Soft to firm
Product handling, coatings, pads and harvester star rollers. Grips and cushions without marking the product.
High impact and abrasive
Drive rollers, washline rollers and conveyor wheels that see dirt, rock, water and long hours. Most rollers and wheels live here.
Rigid and load bearing
Bushings, bearings, heavy duty wheels and parts that carry weight more than they grip, like our 60D AeroPorter wheels.
Hatched ends of the bar fall outside the range we cast. Everyday values are typical figures and real items vary. Shore A and Shore D overlap near 95A, roughly 45D. Not sure what you need? Tell us how the part is used and we will recommend a compound. Ask us
Built for the environment the part runs in
Tell us what the part is exposed to and we match the compound. These are the conditions we formulate for every week.
FDA compliant food contact
Formulations for rollers, scrapers and bumpers that touch produce and food product.
Chlorine and sanitizer washdown
Compounds built to hold up in chlorinated wash water and daily sanitation.
Acidic foods
Tomatoes, peppers, citrus and other acidic product on packing and processing lines.
Water, splashed or submerged
Hydrocoolers, wash lines and wet conveyors.
Heat
Compounds for ovens, dryers and high heat lines. Tell us the operating temperature.
Oils and chemicals
Exposure to lubricants, fuels and process chemicals.
Dirt, rock and abrasion
Field equipment, undercarriage and aggregate, where wear resistance decides part life.
High speed and heavy load
Hard, dynamic compounds for high RPM rollers and load bearing wheels.
A Division of Green Rubber Kennedy Ag
Get a Quote
Send a drawing, a photo of the worn part, or the dimensions and the application. Tell us the environment it runs in and we will match the compound and quote the part.
PMA Regulatory Compliance Program, Level II Compliance